Two mild steel plates of similar thickness, in butt-joint configuration, are welded by gas tungsten arc welding process using the following welding parameters.
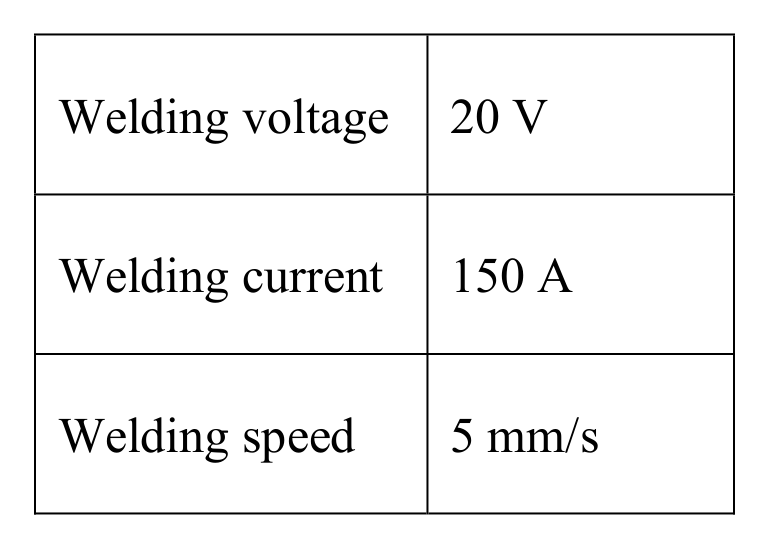 A filler wire of the same mild steel material having 3 mm diameter is used in this welding process. The filler wire feed rate is selected such that the final weld bead is composed of 60% volume of filler and 40% volume of plate material. The heat required to melt the mild steel material is 10 J/mm. The heat transfer factor is 0.7 and melting factor is 0.6. The feed rate of the filler wire is __________ mm/s (round off to one decimal place).